

General engineering
Shafts Flanges Housings
Tool life and consistent machiningExplore tool selectionCUTTING TOOL SOLUTIONS
Start with your current tool and machining conditions. Our tool matching, free sample trials and purchasing support help you assess cutting performance and tooling cost.
Discuss your tools & request samples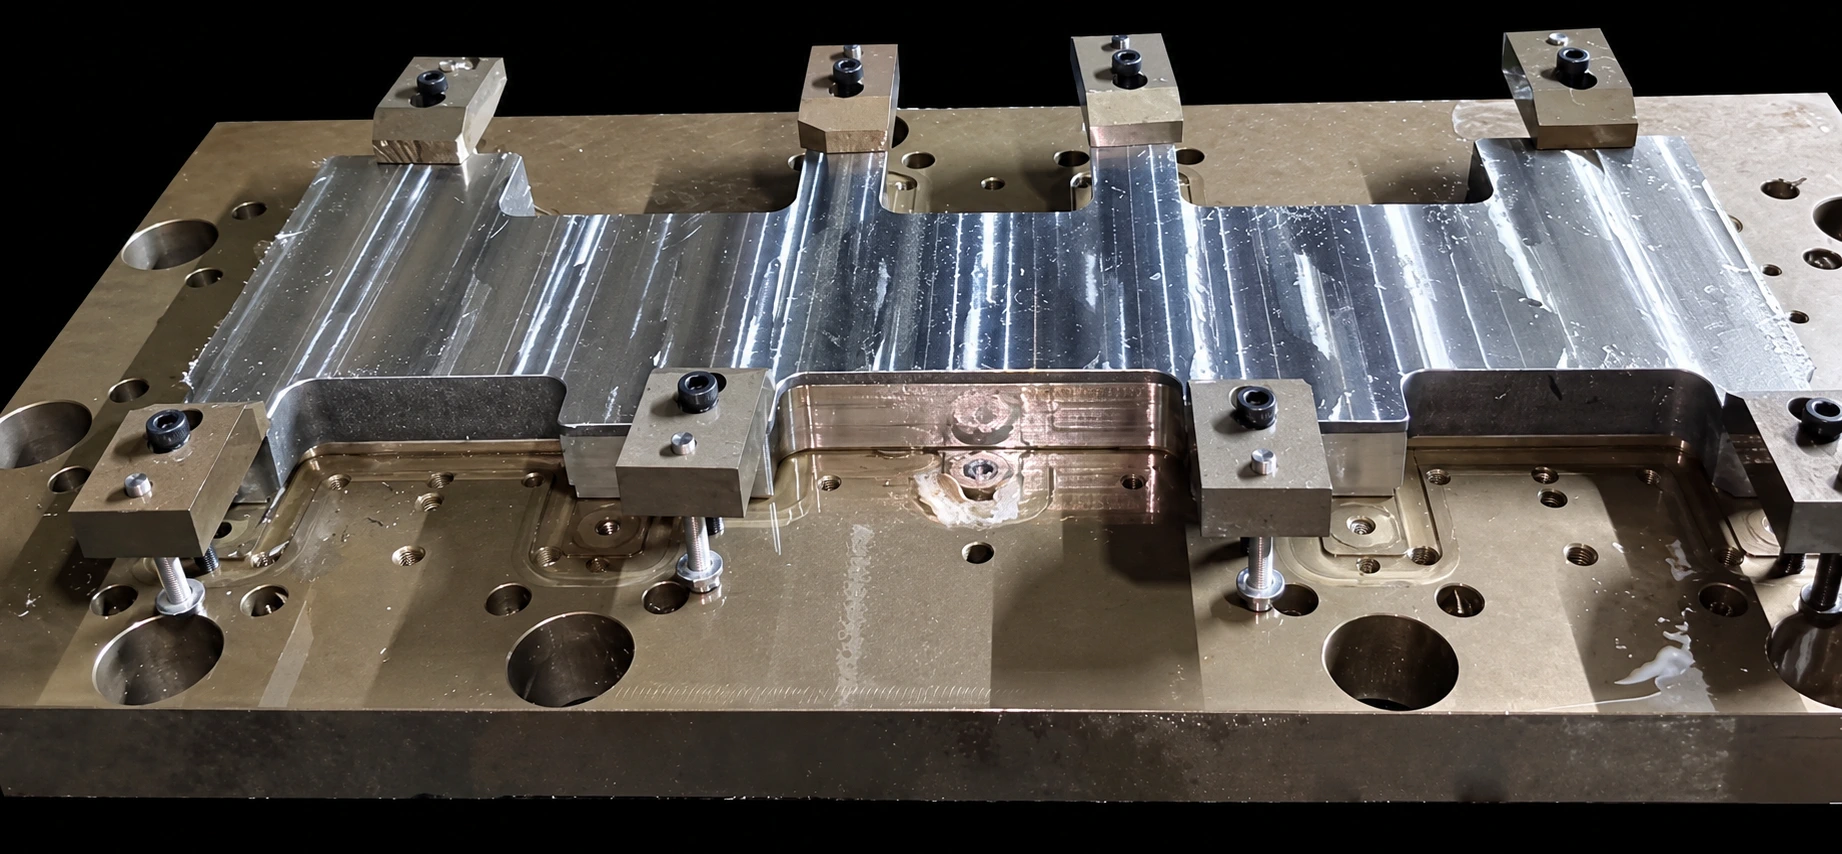
INDUSTRIES & COMPONENTS
Match tool selection to the material and machining requirements.
Shafts Flanges Housings
Tool life and consistent machiningExplore tool selectionPump bodies Shafts Gearbox housings
Cycle time and process stabilityExplore tool selectionCavities Mould inserts Base plates
Roughing, finishing and surface qualityExplore tool selectionBushings Brackets Precision parts
Holemaking and dimensional requirementsExplore tool selectionAPPLICATION SUPPORT
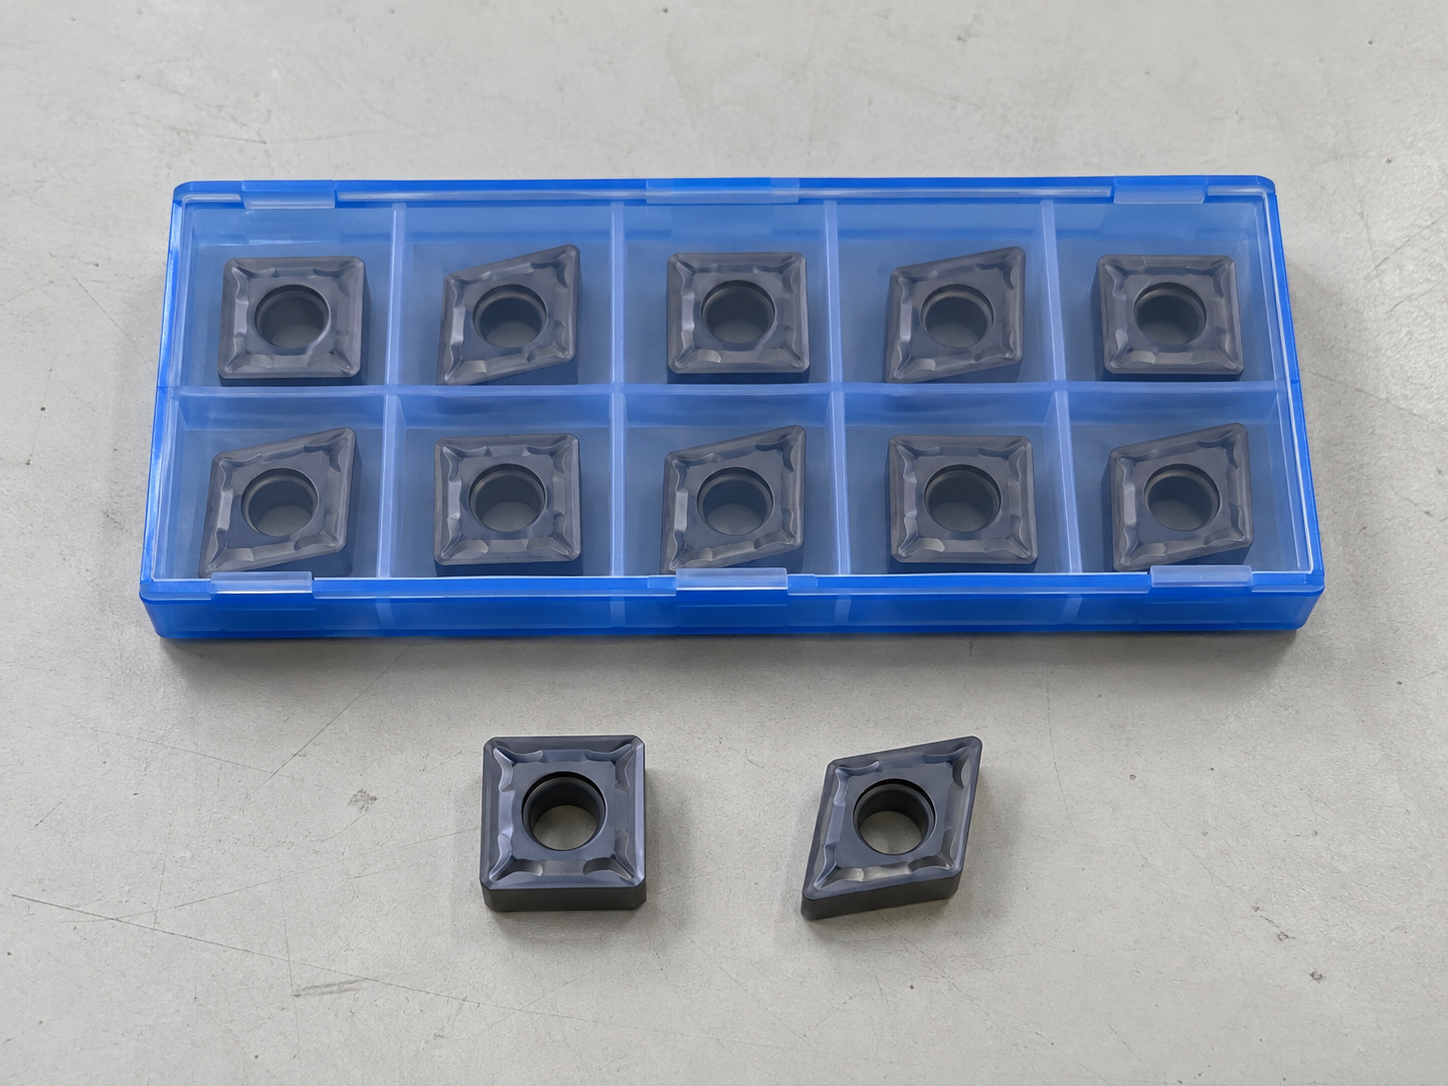
TURNING
External turning and facing of steel and stainless steel
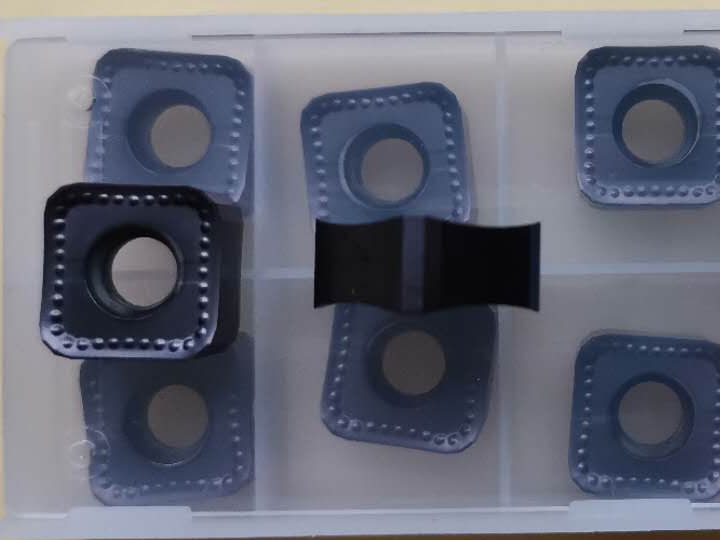
MILLING
Face milling and roughing of cast iron and stainless steel
DRILLING
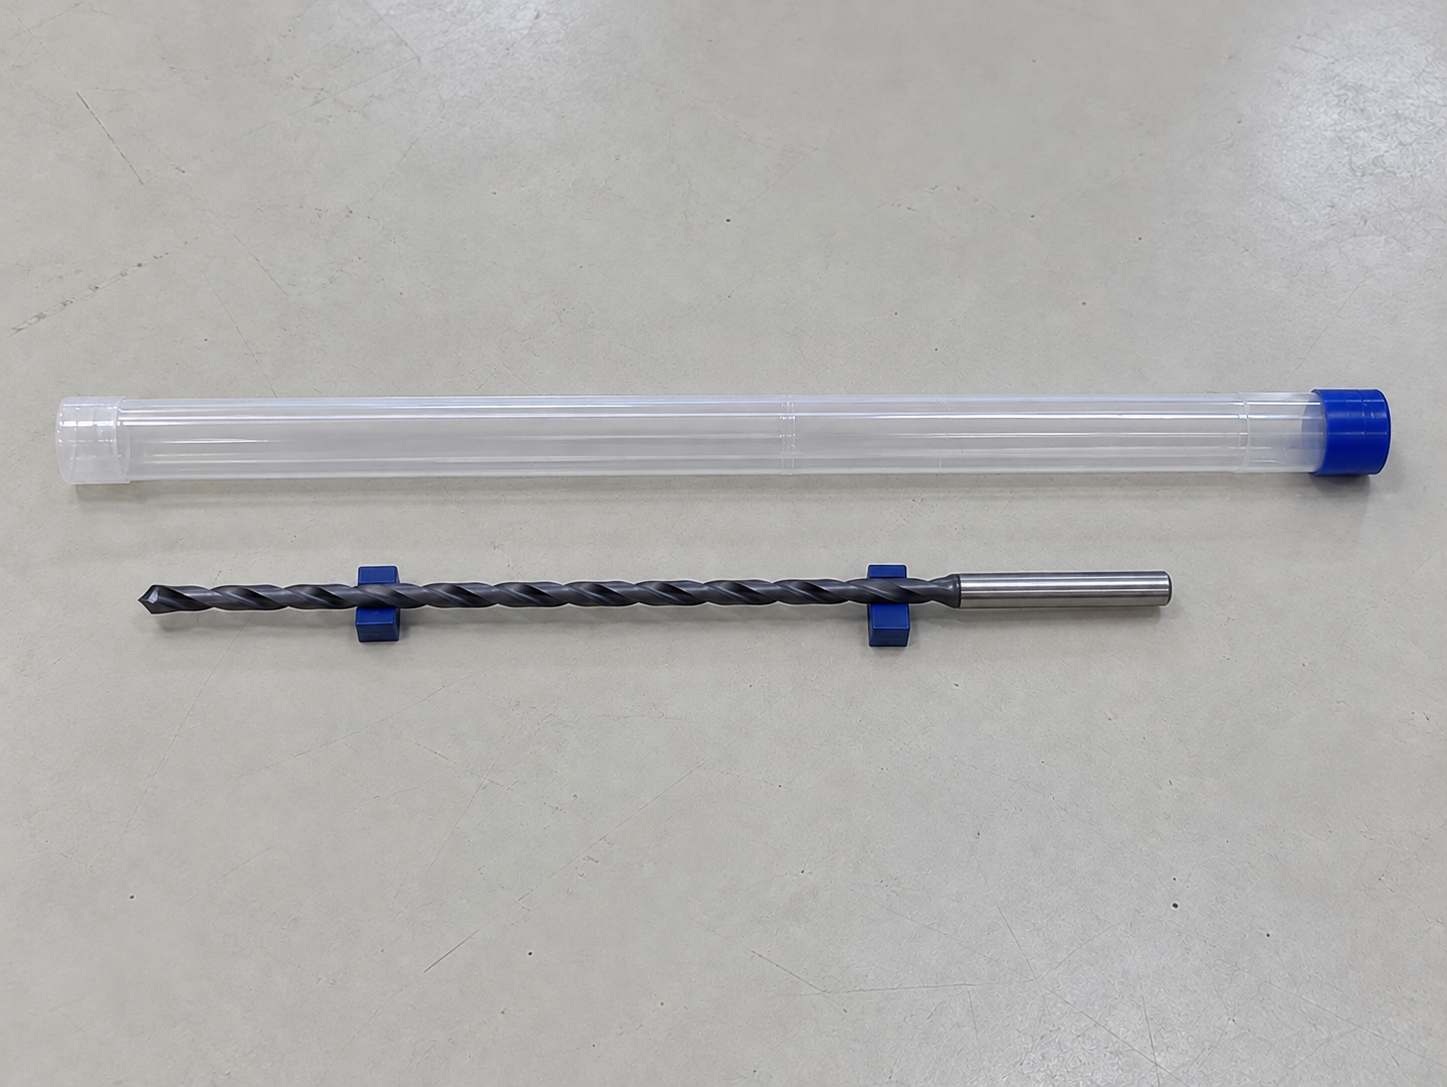
Deep holes in steel shafts, flanges and similar parts
APPLICATION RECORDS
The following application records were supplier-provided. Operating conditions and results are retained from the source records; original supplier model numbers and grades are not disclosed. These cases document historical trials and do not indicate that corresponding HOFNEX models are currently available for sale. Reassess any alternative against your current tool and actual machining conditions.
Compare tool life and machining performance against the existing insert.
Discuss this applicationMachining results were similar, and the trial tool life range overlapped the existing tool's result. Assess the alternative using price and actual output together.
Compare tool life and process stability at the specified hole diameter and depth.
Discuss this applicationBoth trials achieved tool life close to the existing tool. Application trials should also assess chip evacuation, wear and performance during continuous machining.
The two trials used the same recorded spindle speed and feed. Confirm these parameters for your own machine, coolant supply and application before testing.
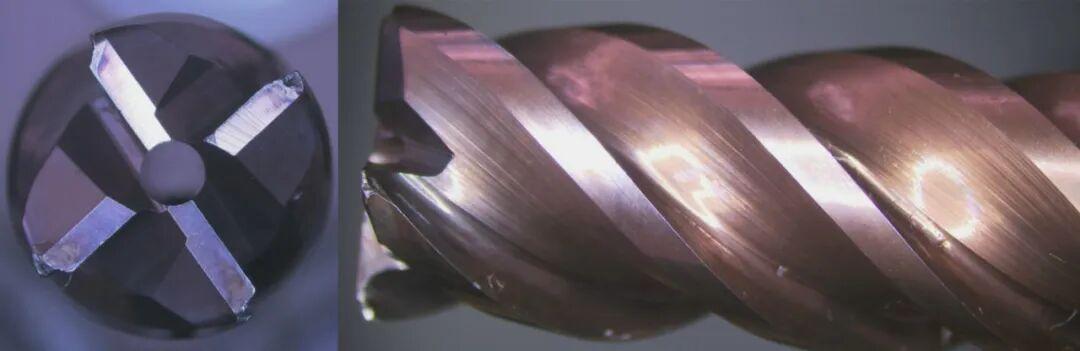
The original record reports 10 parts with the existing tool and 27 with the trial tool. The setup used a D10R0.5 four-flute solid tool, a BT30 machine and oil coolant. Results from different operations should be compared separately.
 Discuss this application
42CrMo at HRC 28; hole diameter 8 mm and depth 235 mm. The existing tool achieved 30 parts with wear or breakage; the trial tool achieved 42 parts with normal wear. The trial used a through-coolant deep-hole drill.
Discuss this applicationTOOL SELECTION & PURCHASING
Share your current tool, material and machining objectives. After confirming a suitable candidate, we can arrange free samples.
Share your tool list, expected quantities and target market to discuss sample selections and supply arrangements.
Free samples can be arranged once the tool specification and application are confirmed.


 Application selection and trials
 Tool lists and volume purchasing